Mixing power and data cables in one cable tray saves steel and installation time, but it couples noise into signal circuits through inductive and capacitive coupling. The practical controls are distance, an earthed metallic divider, separate trays, screened data cables bonded 360°, or fibre optic. Typical separation distances used in industrial projects are 300 mm for unscreened data next to low-voltage power and 600 mm where currents and parallel lengths are larger.
Why separation matters
Two coupling mechanisms dominate in a tray run:
- Inductive (magnetic) coupling — the field around a power conductor induces a voltage in a nearby loop. It scales with the rate of change of current, which is why variable-speed drive output cables, switching devices, and fault currents are the worst offenders.
- Capacitive (electric) coupling — proportional to voltage and to the length of the parallel run, and inversely proportional to separation. An earthed metallic screen or divider intercepts it effectively.
Risk factors, in order of importance: parallel length, separation distance, power circuit current and voltage, whether the power circuit is switched by a drive, whether the data cable is screened, and whether screens are terminated correctly.
What the standards say
- IEC 60364-5-52 / BS 7671 Regulation 528.1 — circuits are grouped into categories (Category 1 power, Category 2 data and telecom). Circuits of different categories may share a wiring system only where every cable is insulated for the highest voltage present, or where separation is provided by distance or by an earthed metallic barrier.
- NEC Article 392 (cable trays) and NEC 300.3(C)(1) — conductors of different systems may occupy the same wiring method only where all conductors are insulated for the maximum voltage applied to any one of them.
- NEMA VE 2 (cable tray installation guidelines) — covers the use of barrier strips and dividers to separate circuit types within a tray.
- TIA-569 (telecommunications pathways and spaces) — widely applied with a 300 mm separation between telecommunications cabling and electrical power conductors; confirm the current edition and the project specification.
- IEC 61000-5-2 — EMC installation and mitigation guidelines, including earthing, bonding, and cable separation by category.
- IEC 61800-3 — EMC requirements for adjustable-speed electrical power drive systems; the practical consequence is that drive output cables are treated as a separate category from signal cables.
- IEE/IEEE guidance (e.g. IEEE 518) — separation distances between power and signal wiring based on voltage, current, and parallel length.
The mechanical and continuity requirements of the tray itself remain under IEC 61537 (cable tray systems) and NEMA VE 1 (metallic cable tray systems).
Separation methods compared
| Method | Typical value used in practice | Best for | Limitations |
|---|---|---|---|
| Separation distance | 300 mm unscreened data vs LV power; 600 mm for higher currents / long parallel runs | Easy to verify on drawings and site | Consumes space; needs discipline over the whole route |
| Earthed metallic divider (barrier strip) in one tray | Full-height divider bonded to the tray; follow NEMA VE 2 and the applicable installation code | Dense routes, retrofits with limited space | Only effective if continuous and properly bonded; check the minimum clearance required by the applicable standard |
| Separate trays | One tray per category, separated by 300 mm or more | New installations with room | More steel and more supports |
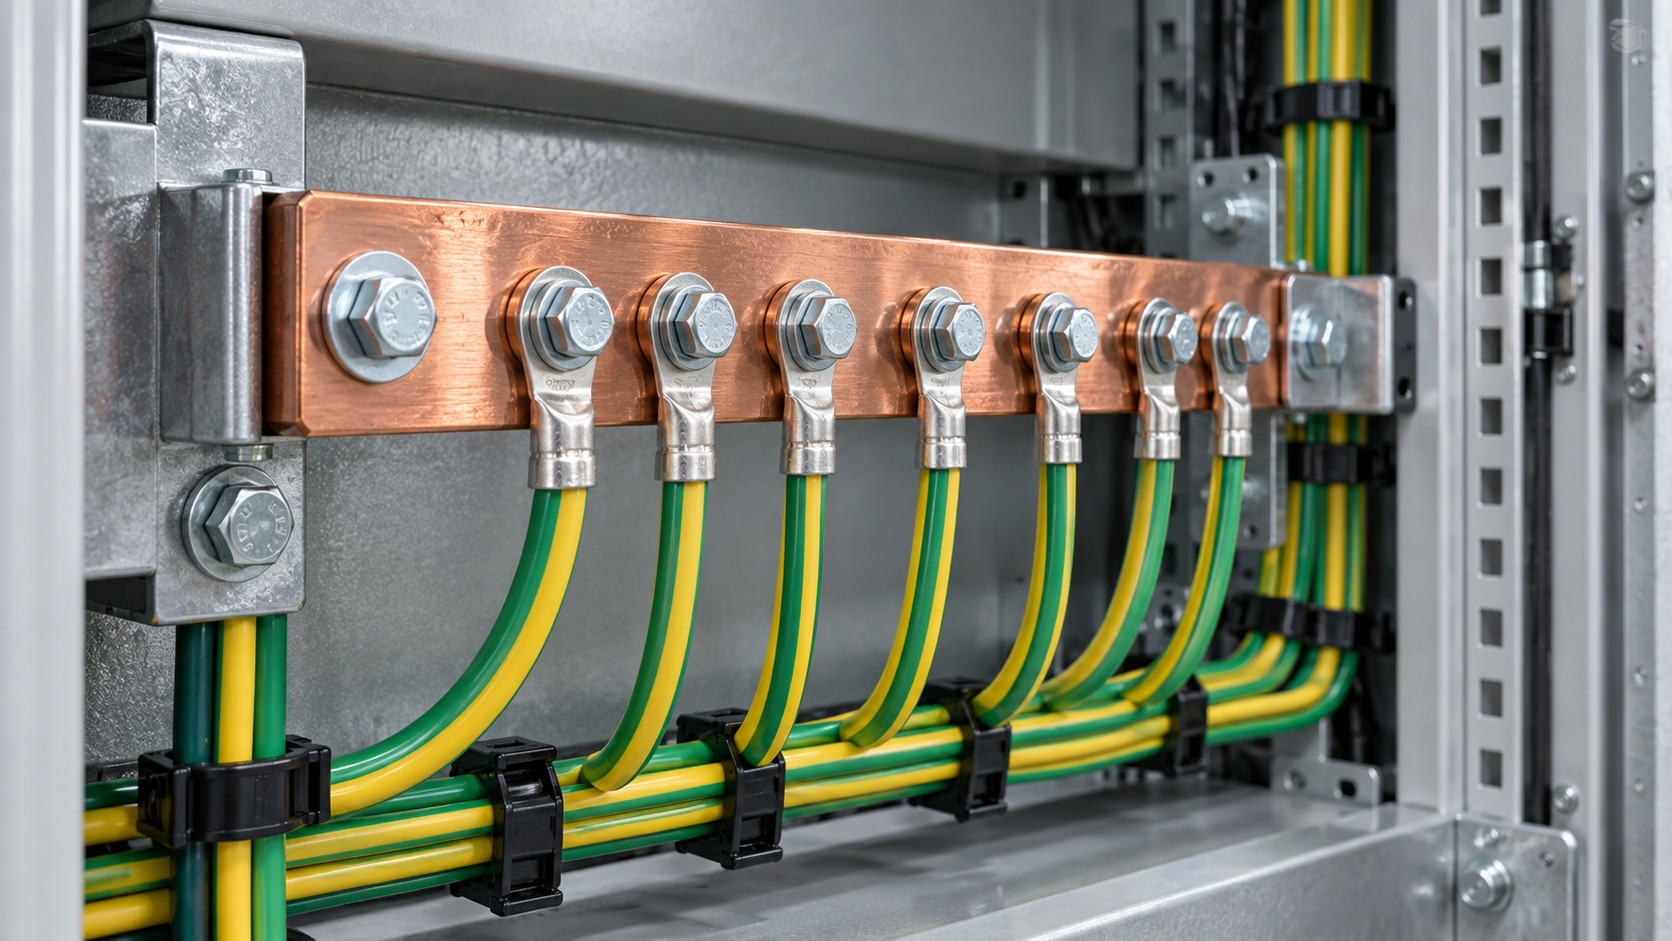
| Screened / shielded data cable | Screen bonded 360° at both ends where a sound bonding network exists | Reduced separation distance | Needs correct glands or clamps; a pigtail termination ruins HF performance |
| Fibre optic | No separation requirement for EMC | Very noisy environments, long runs | Requires conversion equipment and different handling rules |
| 90° crossings | Cross at right angles, keep the crossing short | Where routes must cross | Only helps at the crossing; parallel length is still the risk |
The distances above are typical project values, not universal code limits. The governing distances come from the applicable installation code, the equipment manufacturer’s instructions, and the project EMC plan.
Tray type and divider details
- Ladder and perforated tray: the most common choice for mixed routes; dividers are available as bolt-in or weld-in strips. Bolt-in dividers must be bonded to the tray, not just clipped.
- Wire mesh tray: light and ventilated, but mesh is not a screen — do not assume it provides EMC separation.
- Solid-bottom tray: offers some shielding at low frequency only if the cover is continuous and bonded; a plastic or unpainted cover provides no screen.
- Divider height: use a divider at least as high as the deepest cable it separates, otherwise cables flop over the top.
- Continuity: IEC 61537 covers electrical continuity of tray systems; where the tray forms part of the bonding path, verify continuity by measurement after installation.
Application Scenario: VFD Feeders and Profinet in One Corridor
A plant expansion adds six variable-speed conveyor drives (22 kW and 45 kW, 400 V) and a new Profinet ring, routed from the MCC to the line along the same overhead corridor. The corridor is 1.2 m wide and shared with existing services.
Scenario constraints
- Drive output cables carry PWM waveforms with high dV/dt and are a strong noise source (IEC 61800-3 treats them as a distinct category).
- Existing structure limits the corridor to two new trays.
- Parallel run length is about 60 m — long enough for cumulative coupling.
- The line runs continuously; an EMC fault would stop production.
Selection approach
- Two trays, not one: drive/motor cables in a dedicated steel tray; Profinet and other data in a second tray. Place them 300 mm apart; increase to 600 mm if the corridor allows.
- Screened motor cable with symmetrical construction, screen bonded 360° to the drive PE terminal and to the motor frame using conductive glands.
- Screened data cable (S/FTP or F/UTP as required by the network design), screen bonded 360° at both ends, with the bonding network in place.
- Crossings: where the data route must cross power, cross at 90° and keep the crossing as short as possible.
- Bonding: both trays bonded to the installation’s equipotential bonding system; continuity measured, not assumed.
- Separate conduit or tray for the last drop to each drive keypad and each network cabinet.
- Document it: record the route, separations, cable types, and screen termination method in the as-built EMC plan.
Common mistakes
- Running data cables in the same tray as VFD output cables “for a few metres” — the few metres are often the parallel section that matters.
- Terminating a cable screen with a long pigtail; at high frequency the pigtail inductance defeats the screen.
- Using a plastic divider or a plastic tray cover as if it were a screen.
- Assuming wire mesh provides shielding.
- Bonding data screens at one end only, without checking the manufacturer’s instruction and the bonding network design.
- Ignoring crossings: allowing 30 m of parallel run at 50 mm separation because “they only cross once”.
- Leaving the divider unbonded, or ending it before the end of the run.
Acceptance checkpoints
- Route inspection against the separation drawing; measure the actual distance at several points, not just at the start.
- Divider continuity: verify that barrier strips are bonded to the tray and continuous along the run.
- Tray continuity: measure resistance across joints and confirm the bonding arrangement.
- Screen terminations: verify 360° clamps or glands at both ends, no pigtails on HF-critical circuits.
- Separation at crossings verified at 90°.
- Functional check: network error counters or diagnostic counters monitored during drive operation; drive operates at full load without nuisance trips.
- Documentation: as-built route drawings, cable schedule with types, and screen-termination records.
Selection checklist
- List every circuit category on the route: LV power, drive output, control, instrumentation, data, telecom.
- Decide the separation strategy per pair: distance, divider, separate tray, or fibre.
- Fix the distances in a table in the specification, with values taken from the applicable code and the equipment manufacturer.
- Choose tray type and confirm the divider is available for that type and is bondable.
- Confirm cable types: screened drive cable, screened data cable, rating for the environment.
- Confirm load and span for each tray (IEC 61537 or NEMA VE 1), remembering that dividers and extra trays add weight.
- Confirm the bonding and earthing arrangement for trays, screens, and equipment.
- Plan the crossings.
- Decide how separation will be inspected and documented.
Quality inspection checkpoints
- Tray and divider material, thickness, and coating verified against the order.
- Divider height checked against the deepest cable.
- Continuity tested across tray joints and divider fixings; results recorded.
- Cable schedule checked: screened cable supplied where specified, screen construction as specified.
- Glands and clamps: conductive, correctly sized, and fitted to give 360° contact.
- Fill and support: cables supported at the intervals required, dividers not deformed by cable weight.
- Photographic record of the route before covers or ceilings close.
How to evaluate a supplier
- Ask whether the tray range includes bondable dividers and barrier strips for the exact tray type and width.
- Ask for the declared working load and span to IEC 61537 or NEMA VE 1, including the effect of accessories.
- Ask for continuity performance data for the tray system and its joints.
- Ask for the finish and material specification, and the coating’s suitability for the environment.
- Ask whether they supply matched accessories: bends, tees, risers, drop-outs, and covers that keep the divider path continuous.
- Ask for documentation: load tables, installation instructions covering bonding, and material declarations.
Frequently Asked Questions
1. What is the minimum separation between power and data cables?
There is no single universal number. Project practice commonly uses 300 mm for unscreened data next to LV power and 600 mm for higher currents or long parallel runs; an earthed metallic divider is accepted in place of distance under many installation rules. Always check the applicable code and the equipment manufacturer’s instruction.
2. Can power and data share the same tray?
Sometimes. IEC 60364-5-52 / BS 7671 Regulation 528.1 allows it where every cable is insulated for the highest voltage present, or where an earthed metallic barrier separates the categories. NEC 300.3(C)(1) has a similar “insulated for the highest voltage” condition.
3. Does a divider have to be earthed?
Yes for EMC purposes. An unbonded metallic divider does not provide a low-impedance return path. Bond it to the tray and confirm continuity.
4. Is wire mesh tray a shield?
No. Mesh is open by design; it provides no meaningful shielding at the frequencies of concern.
5. Should data cable screens be earthed at one end or both?
Where a sound equipotential bonding network exists, HF performance is best with 360° bonding at both ends. Where low-frequency earth loops are a concern, follow the equipment manufacturer’s instruction and IEC 61000-5-2 guidance.
6. How much does parallel length matter?
A great deal — coupling accumulates along the parallel run. Reducing parallel length is often more effective than adding separation.
7. Is fibre worth it?
In very noisy environments or where separation cannot be achieved, fibre removes the EMC problem entirely. It costs more in termination and test equipment but avoids recurring interference faults.
Planning a Mixed Power and Data Route?
BANGE Electric supplies ladder, perforated, and wire mesh cable tray with matched dividers and accessories, and can provide declared load and span data to IEC 61537 or NEMA VE 1. Share your route drawing, cable schedule, and separation requirements through the cable tray buyers guide or contact our engineering team.
Requirements may vary by application, market, and applicable standard.